Engineered Heavy-Duty Storage & Pallet Racking Portfolio
Direct-from-manufacturer heavy-duty storage configurations designed for rapid forklift handling, vertical modularity, and high-density warehouse throughput.
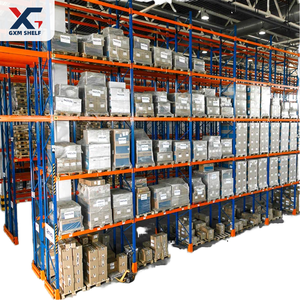
Heavy Duty Boltless Selective Pallet Rack Rivet Shelving Steel Warehouse Storage System with ESD Protection Epoxy Powder Coated
Inspect Technical Spec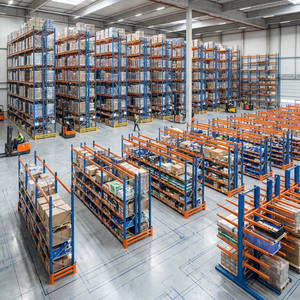
Industrial Heavy Duty Pallet Racking System Adjustable Warehouse Storage Shelving Q235B Steel Selective Rack For Cargo Handling
Inspect Technical Spec
Long Span Warehouse Racking Heavy Duty Boltless Adjustable 500kg/Layer 5-Tier Steel Rack Industrial
Inspect Technical Spec
Industrial Heavy-Duty Multi-Level Steel Shelves Metal Rack And Warehouse Pallet Racking System
Inspect Technical Spec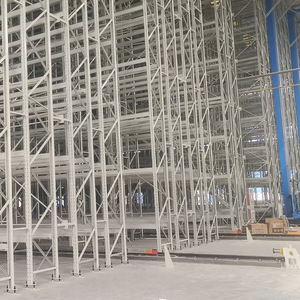
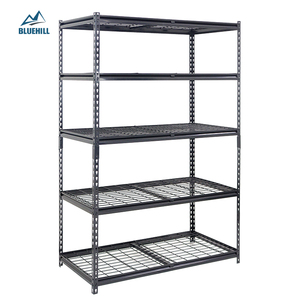
Hospital Shelves Slotted Angle Bar Steel Steckregal Metal Regalsystem Display Rack/Storage Rack with Particle Shelves
Inspect Technical Spec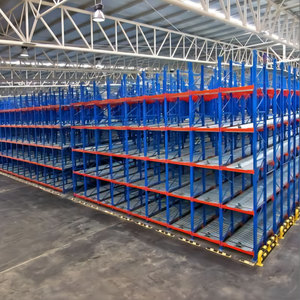
Durable Heavy Duty Adjustable Steel Gravity Flow Racking System Storage Racks 2025 Trending Warehouse Pallet Flow Roller Shelf
Inspect Technical Spec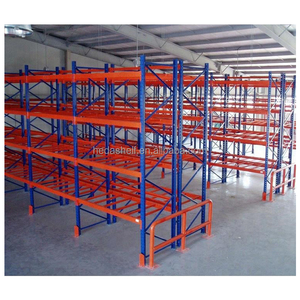
Wide Aisle Pallet Racking Heavy Duty Metal Rack Double Deep Clothes Racking System for Warehouse
Inspect Technical SpecHeavy Duty Engineering Built On 50+ Years of Single-Source Accountability
As a dedicated OEM/ODM manufacturer of industrial pallet stacking racks and heavy structural warehouse systems, our production ecosystem unifies engineering calculation, robotic MIG welding, hot-dip galvanization, and epoxy-polyester electrostatic powder coating under one accountable roof.
Eliminate intermediary markups and configuration bottlenecks. Our certified structural engineers partner directly with warehouse managers, logistics 3PL contractors, cold-storage developers, and automotive Tier-1 suppliers to fabricate bespoke post pallets, portable stacking racks, coil storage cradles, and heavy-duty frame systems customized to exact facility footprints.
RMI & ANSI MH16.1 Certified
Every rack column, post socket, and cross brace meets rigid structural buckling ratios and seismic load tolerances.
85% Nesting Efficiency
Removable post and collapsible corner systems slash reverse-logistics freight volumes and maximize unused floor space.
Q235B & Q355B Steel Mills
Direct mill sourcing guarantees traceable metallurgical composition, high yield limits, and impact absorption.
Full Turnkey OEM Customization
Tailored post heights, cup feet, fork stirrups, mesh decking, and dynamic tare capacities engineered to spec.
OEM/ODM Production Benchmark
- Structural Raw MaterialPrime Q235B / Q355B Carbon Steel
- Stacking Dynamic Capacity1,000 kg – 2,500 kg / Unit
- Static Stack ElevationUp to 4 – 6 Tiers High
- Weld Integrity TestingAWS D1.1 Ultrasonic & Penetrant
- Deflection Ratio StandardL/200 Under Dynamic Working Load
- Surface TreatmentPolyester Powder Coat / Hot-Dip Galvanized
- Anti-Corrosion Salt Spray500 – 1,000+ Hours ASTM B117
- Forklift Handling Access4-Way Entry with Guide Stirrups
Heavy Duty Pallet Stacking Racks: Technical Selection Matrix
Compare mechanical structural designs, load dynamics, footprint utilization, and warehouse operational performance across primary pallet rack configurations.
| Rack Architecture | Dynamic / Static Load | Floor Space Efficiency | Selectivity & Access | Nesting & Reconfiguration | Best Suited Application |
|---|---|---|---|---|---|
| Modular Post Pallet Stacking Racks | 1,500 kg dynamic / 6,000 kg static (4-high) | Ultra High (Dense Bulk) | Block Stacking / Batch FIFO-LIFO | Removable posts yield 80% empty storage savings | Seasonal inventory, tires, bulk bags, automotive stampings, leased warehouses |
| Structural Bolted Selective Rack (SK3000) | 2,000 kg – 4,000 kg per beam level | Moderate (Dedicated Aisles) | 100% Immediate Direct Access | Fixed footprint; bolted reconfiguration | Heavy distribution centers, cold-storage freezers, high forklift impact zones |
| Boltless Tubular Pallet Rack (SK2000) | 1,000 kg – 2,500 kg per beam level | High Vertical Utilization | 100% Pallet Selectivity | Fast tool-free teardrop pin adjustment | Retail logistics, e-commerce fulfillment, consumer goods, FMCG sorting hubs |
| Dynamic Gravity Flow Roller Racking | 1,000 kg per pallet lane | Maximum Depth Density | Strict FIFO by Lane | Fixed flow incline with centrifugal brakes | Perishable food & beverage, cold chain distribution, strict expiration lot control |
| Double Deep Reach Racking System | 1,200 kg – 2,000 kg per position | High (Aisle Elimination) | 50% Immediate Selectivity | Requires pantograph deep-reach forklifts | Identical SKU manufacturing buffers, dry goods storage, bulk carton staging |
Future Procurement Trends in Industrial Stacking Racks (2025–2030)
How global procurement officers, supply chain executives, and distribution facility planners are redefining heavy-duty racking investments.
Flexibility Over Fixed Civil Anchors
Tenant-leased distribution hubs increasingly avoid floor-anchored stationary uprights that cause substantial decommissioning expenses. Portable stacking racks allow zero floor slab damage, enabling operators to transform empty floor space into a multi-tiered warehouse overnight and collapse the entire system when inventory contracts.
Scope 3 Carbon Accounting & Circularity
Enterprise procurement directives mandate transparent carbon footprints for capital expenditures. Heavy-duty Q235B/Q355B steel post pallets constructed with electric-arc furnace (EAF) recycled scrap metal and finished with VOC-free powder coatings are outperforming timber pallets and single-use wooden crates in global ESG audits.
AGV & AMR Autonomous Interoperability
Stacking racks are evolving from manual forklift handling to automated guided vehicle (AGV) compatibility. B2B buyers now specify chamfered nesting cup bases, high-contrast optical guidance targets, laser-cut fork positioning stirrups, and tighter dimensional tolerances (±1.5mm) to support uncrewed automated material handling.
Technological Breakthroughs in Heavy Duty Stacking Rack Engineering
Modern industrial supply chains demand extreme structural safety, lighter structural tare weights, and corrosion resilience under harsh operating environments like sub-zero cold storage and coastal salt air. Our OEM/ODM engineering division implements four pivotal manufacturing developments:
1. Finite Element Analysis (FEA) and Micro-Alloyed High-Yield Steels
By transitioning from conventional mild steel to low-alloy, high-strength cold-rolled and hot-rolled steels (such as Q355B and micro-alloyed structural tubes), our stacking racks achieve a 22% increase in allowable buckling strength while lowering overall unit tare weight. Each custom stacking rack design is subjected to rigorous 3D finite element simulation (FEA) under static load, dynamic seismic acceleration, and accidental forklift mast impact loads to eliminate stress concentration nodes at base cups and upright welds.
2. Automated Robotic MIG Welding with Certified Penetration Profiles
Weld failure is the single greatest risk factor in multi-tiered stacking racks. Our ISO 3834-certified manufacturing lines employ 6-axis robotic welding stations using digital pulsed synergic arc welding. This guarantees 100% repeatable root penetration along the heavy cup sockets, vertical post receivers, and tubular perimeter rails. Non-destructive ultrasonic and liquid penetrant testing validates that our welded joints sustain dynamic shock loadings from heavy forklift drop cycles without micro-fissuring.
3. Next-Generation Hybrid Surface Treatments: Hot-Dip Galvanizing & Dual-Coat Epoxy
For sub-zero cold-storage facilities (-30°C) where condensation leads to catastrophic structural rusting, standard single-coat paint fails within 24 months. Our OEM production lines offer hot-dip galvanization according to ISO 1461 / ASTM A123, providing a metallurgical zinc-iron alloy barrier over 85 μm thick. For dry distribution warehouses, our 7-stage phosphate pre-treatment followed by high-adhesion electrostatic thermosetting epoxy-polyester powder coating delivers supreme resistance against scratching, abrasion, and chipping during intense daily forklift loading.
4. Modular Collapsible Geometries & Reverse Logistics Economics
Freight expense often represents up to 30% of total racking procurement cost. Our newly engineered nesting post pallets and detachable corner-tube racks allow up to 45 disassembled units to nest securely into a single standard 40ft High-Cube ocean freight container. In regional closed-loop supply chains, returning empty racks at a 5:1 volume reduction optimizes backhaul logistics and saves thousands of dollars annually per freight corridor.
Frequently Asked Questions for OEM/ODM Buyers
Authoritative technical answers covering steel specifications, international load compliance, customization cycles, and quality verification.
What is the standard yield strength difference between Q235B and Q355B steel for stacking racks?
Q235B carbon steel has a minimum nominal yield strength of 235 MPa and a tensile strength of 370–500 MPa, making it the globally accepted, cost-effective standard for general selective pallet racks and light-to-medium stacking units (up to 1,200 kg per tier). In contrast, Q355B (equivalent to European S355JR and ASTM A572 Grade 50) delivers a yield strength of 355 MPa and tensile strength of 470–630 MPa. We recommend Q355B for high-density heavy stacking racks carrying 1,500–2,500 kg per unit, multi-tier post racks stacked 5–6 levels high, or installations in active seismic zones where superior energy dissipation and plastic deformation resistance are required.
How do you verify the safe stacking capacity and seismic rating of custom OEM post pallets?
All custom OEM/ODM racking designs undergo dual verification: structural simulation and destructive laboratory testing. First, our engineering team performs 3D Finite Element Analysis (FEA) compliant with RMI (Rack Manufacturers Institute) ANSI MH16.1, EN 15512, and AS 4084 standards, incorporating P-Delta second-order geometric non-linearity and regional seismic ground acceleration factors (Ss and S1). Second, physical prototypes are subjected to destructive static load presses up to 2.0x safety factor (twice the rated load) for 48 hours to confirm zero permanent plastic deformation, as well as 1.25x dynamic tilt table evaluations to verify cup-to-post engagement stability.
What custom options can be specified during the OEM/ODM tooling and design phase?
We provide full-spectrum ODM/OEM bespoke manufacturing: 1) Dimensional Geometries: Custom base widths, depths, and vertical clear heights to accommodate oversize non-standard goods like master rolls, raw textile coils, automotive engine cradles, and irregular cargo. 2) Base Flooring: Welded heavy wire mesh decking (50x50mm or 100x100mm), solid steel sheet plate (1.5mm to 3.0mm), perforated ventilation plate, or cross-support bars. 3) Post Mechanisms: Removable drop-in tubular posts, screw-lock collars, spring-loaded quick-release pins, or fold-down hinged corners. 4) Forklift Interfaces: 2-way or 4-way full fork entry channels, captive fork guide stirrups, and anti-skid base skid runners. 5) Corrosion Finishes: Custom RAL powder coating colors for SKU department color-coding, zinc electroplating, or heavy industrial hot-dip galvanizing.
What are the packaging methods and lead times for high-volume ocean container shipments?
Standard lead times for full container load (FCL) orders average 3 to 4 weeks from approved engineering drawings and sample sign-off. Post pallet bases are nested and secured with high-tensile polyester strapping onto timber or steel skids, wrapped with multi-layer waterproof stretch film, and fitted with high-density corrugated corner protectors to prevent transit rub damage. Removable vertical posts are bundled in designated steel cages or steel strap bundles sized for seamless forklift devanning at receiving docks. A single 40ft HQ container typically accommodates between 180 and 420 nested pallet bases depending on dimensions and post options.
Why choose custom stacking post racks over permanent conventional selective pallet racks?
While stationary selective pallet racking excels in dedicated distribution centers requiring 100% individual SKU selectivity, portable stacking post racks offer distinct operational advantages: 1) Zero Building Anchoring: No concrete expansion bolts into warehouse floor slabs, avoiding slab damage and complex civil building permitting. 2) Dynamic Reconfigurability: Stack racks can be moved with loads still inside, serving as both storage rack and shipping cradle simultaneously. 3) Bulk Seasonal Density: Eliminate forklift travel aisles during peak storage cycles by block-stacking up to 4–6 tiers high. When off-season arrives, dismantle the posts to nest the bases, reclaiming up to 80% of warehouse floor space for alternative operations.
Partner with a Certified Heavy-Duty Racking Manufacturer
Request direct factory pricing, structural FEA calculations, and custom prototype samples tailored to your exact load profile and warehouse dimensions.